Choosing a Tube Mill Pipe Making Machine is not just a matter of comparing advertised speeds or prices. The right line must match your pipe dimensions, material, production volume, and available floor space. A machine designed for thin-wall stainless steel may not suit heavier carbon steel work. Small details matter.
Before requesting quotations, define your target outside diameters, wall thicknesses, and tolerance requirements. Consider the full production path, including forming, high-frequency welding, sizing, and cutting. Ask how quickly the line can change between sizes, and what tooling or setup time each change requires. A fast machine is less useful if frequent changeovers slow the whole shop.
The seven tips in this guide help buyers assess capacity, weld quality, automation, tooling, maintenance, supplier support, and total operating cost. Look beyond brochure figures. Request test-run details, inspect sample pipes, and confirm which components and services are included. A brochure can make every line look precise; real production is less tidy. That deserves a closer look. Verify performance against your own material and product specifications, rather than relying on broad claims. The best Tube Mill Pipe Making Machine is the one that can meet your requirements consistently, with a support plan your team can actually use.
Before comparing tube mill pipe making machines, write down the pipe you need to produce. Specify the material, outside diameter, wall thickness, and target length. Include acceptable tolerances, too. A pipe measuring 40 millimeters across with a 1.5-millimeter wall needs different forming and welding settings from a heavier product. Small differences matter.
Consider the full range of products, not only your most common size. If sizes vary, record the minimum and maximum diameters and thicknesses. Note whether the machine must handle stainless steel, carbon steel, or another material. Then estimate output in finished pipes per hour, including time for coil changes and adjustments. A quoted speed may assume ideal conditions. Real production includes interruptions.
Think about the downstream process as well. Will pipes be cut to fixed lengths, deburred, or inspected in line? These steps can limit actual output more than the mill itself. Bring sample drawings and material specifications when discussing machine capacity. That helps suppliers identify practical constraints, such as roll changes or limited thickness ranges. Specifications may still need revision after trials. That is normal. A little uncertainty is better than pretending every detail is settled.
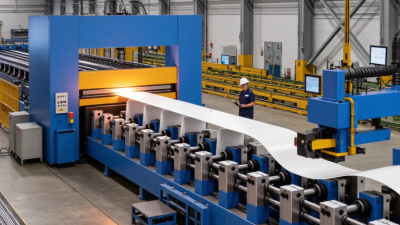
A tube mill should be configured around your actual coil stock, not an ideal sample in a catalog. Start with material grade, yield strength, thickness range, strip width, and coating. These values affect forming loads, roll design, and drive capacity. Small details matter. Thin, high-strength strip may spring back more than expected, while thick mild steel can require greater forming force. Ask the machine builder to check the proposed range against material certificates and sample coils.
Consider how each material behaves. Carbon steel, stainless steel, and aluminum form and weld differently. Stainless steel may need careful roll-surface control to limit pickup and visible marks. Aluminum needs clean handling and suitable tooling to prevent scratches. Confirm the welding process, seam position, tube diameter, and wall thickness together. A mill rated for one size may not maintain tight tolerances across every material. Check changeover time, too.
Define the full material range before selecting forming stands, roll tooling, motors, and welding equipment. Request trial runs with the thinnest and thickest planned coils, as well as the hardest grade. Measure bead consistency, ovality, straightness, and surface finish after cooling. Keep samples. If future grades are uncertain, allow adjustment capacity without paying for range you will not use. No chart captures every coil. Review defects with operators; a small edge wave may point to a mismatch in strip preparation or forming sequence.
7 Tips for Choosing a Tube Mill Pipe Making Machine
Compare Forming Capacity, Speed, and Product Accuracy
Start with the pipe range you actually sell, not the machine’s maximum capacity. Record each diameter, wall thickness, material grade, and section shape. Then check whether the forming stands and welding system can handle your heaviest specification without pushing the line beyond its limits. The World Steel Association’s World Steel in Figures 2024 reports 1,882.6 million tonnes of crude steel production in 2023. That scale makes material compatibility worth checking carefully, even for a single production line. Ask suppliers to demonstrate your own material and dimensions. Numbers need context. A quoted maximum speed may describe steady running, not coil changes, setup, or rejected starts.
Compare output at the quality level your customers require. A faster line is not useful if pipe diameter, seam position, or straightness drifts during a long run. Request measured samples at different speeds, and review how the machine handles size changes. The U.S. Department of Energy’s Improving Motor and Drive System Performance sourcebook estimates that motor-driven systems use about 70% of U.S. industrial electricity. This is a useful reminder to compare drive efficiency and operating load alongside metres per minute. Check real samples. Also inspect the measuring method: a tolerance figure without a defined gauge or test condition is hard to verify. One detail is easy to miss: your plant’s coil handling and operator routines can affect actual output as much as the mill specification.
Compare forming capacity, production speed, and product accuracy
Use the tube size range as a starting point when comparing forming capacity. Larger-diameter ranges may run at lower line speeds, while achievable dimensional accuracy depends on material, wall thickness, tooling, and process control. Values shown are illustrative planning benchmarks, not guaranteed machine specifications; confirm requirements with suppliers and applicable product standards.
A tube mill’s tooling should match the pipe sizes and materials you plan to run, not just the machine’s maximum capacity. Check the roll stands, forming rolls, sizing tools, and weld-zone components against your actual product range. Ask how long a changeover takes and which adjustments need an experienced operator. Small details matter. A poorly matched tool set can leave marks, uneven seams, or excessive scrap.
Automation can improve consistency, but more controls do not automatically mean easier operation. Review how the line handles strip feeding, speed changes, and shutdowns. Can an operator quickly see an alarm’s cause? Are settings saved for repeat production runs? A factory trial using your material is more revealing than a polished demonstration. It may expose awkward changeovers or controls that feel less intuitive than expected.
Quality controls should check the pipe throughout production, not only at the end. Look for practical checks on dimensions, weld condition, and surface finish, with clear records for each run. Ask which measurements are automatic and which depend on manual sampling. That can be costly. Also confirm that gauges are maintained and operators know what action to take when readings drift. A reliable mill supports repeatable checks, but people still need time to interpret the results.
| Tip | Evaluation Area | What to Check | How to Verify |
|---|---|---|---|
| 1. Define the product range | Tube specifications and materials | Confirm the required tube outside-diameter range, wall-thickness range, length, material grades, and incoming strip dimensions. Check that the proposed line covers the full product mix, not just one sample size. | Compare the machine’s documented operating range with your product drawings and material specifications. Request a written capability matrix for each product family. |
| 2. Evaluate the forming and sizing tooling | Roll design, setup, and changeover | Ask how the roll passes support forming, welding preparation, and final sizing. Review the number of stands, roll adjustment method, tooling storage, and which tooling components must be changed between sizes. | Review tooling drawings and a changeover procedure. Where practical, observe a size change and check the resulting tube for profile consistency and surface marks. |
| 3. Match the welding system to the application | Welding process and seam control | Confirm the proposed welding process is suitable for the material, thickness, diameter, and production requirements. For high-frequency welded lines, review power capacity, weld-zone setup, impeder arrangements where applicable, and operating controls. | Ask for a trial using representative material. Review weld setup records and specify the seam inspection or testing method required by the applicable product standard. |
| 4. Check automation and operator controls | PLC, HMI, drives, and production data | Review recipe storage, speed coordination between sections, alarm and fault history, operating parameters, and access controls. Confirm which settings operators can adjust and which are protected. | Request a demonstration of recipe selection, alarm handling, and retrieval of production data. Verify that electrical drawings, control documentation, and training are included in the scope. |
| 5. Assess cutting and length control | Cutoff method and finished lengths | Check whether the cutoff system suits the intended line speed, tube section, wall thickness, and required end condition. Confirm the length-measuring method and the acceptance tolerance for finished pieces. | Run a sample production test and measure a defined sample of cut lengths. Record the measuring method and results against the agreed product specification. |
| 6. Specify quality controls and safety features | Inspection, testing, and machine protection | Identify required checks for dimensions, straightness, weld integrity, and surface condition. Review guarding, emergency stops, interlocks, and safe access around rotating, moving, and hot sections. | Agree on a quality-control plan based on the applicable product standard and customer requirements. Inspect safety devices during acceptance testing and document test results. |
| 7. Confirm commissioning and lifecycle support | Acceptance testing, maintenance, and spares | Clarify installation responsibilities, operator and maintenance training, preventive-maintenance schedules, recommended spare parts, and technical support arrangements. | Set measurable acceptance criteria before purchase, including the test material, product sizes, run conditions, inspection records, and required documentation. |
Machine capability and acceptance limits depend on the product, material, applicable standards, and agreed operating conditions. Confirm all specifications in the purchase contract.
A tube mill should be judged by more than its rated output. Look closely at guarding around the forming section, accessible emergency stops, and clear isolation points for maintenance. Ask operators to demonstrate threading and a size changeover. These tasks can expose awkward reaches or pinch points that a smooth production run may hide. Small details matter. Also check whether noise, coil loading, and scrap removal have been considered in the work area. A safe machine still depends on practical procedures and operator training.
Service support affects uptime long after installation. Ask what troubleshooting help is available, how quickly common wear parts can be supplied, and whether technicians can guide setup remotely. Get service terms in writing. Then estimate total ownership cost, including tooling, electricity, consumables, training, installation, and expected downtime. A low purchase price may not stay low when changeovers require extra labor or specialized parts. A spreadsheet will still miss something; production schedules and local support can change the calculation. That uncertainty deserves attention before committing.